Agricultural production generates enormous amounts of straw and other crop residues every year. Wheat straw, rice straw, corn stalks, barley straw, sorghum stalks, and similar materials are often left in fields, burned, composted, or used as low-value animal bedding. While these approaches can be useful in some situations, a large portion of agricultural waste still remains underutilized.
Straw pelletizing provides another way to use these residues. By processing loose and bulky straw into dense cylindrical pellets, agricultural waste can be converted into a more convenient solid biomass fuel. The pelletizing process improves bulk density, simplifies transportation and storage, and produces a more standardized fuel suitable for biomass heating systems and industrial boilers.
A properly designed straw pellet production line can combine shredding, drying, grinding, pelletizing, cooling, screening, and packaging into one continuous process. At the center of this system is the pellet press, which applies mechanical pressure to compress prepared straw through die holes and form compact pellets.
This article explains how straw pelletizing turns agricultural waste into fuel, how the process works, what equipment is required, and what factors should be considered when designing a straw fuel pellet production line.
What Is Straw Pelletizing?
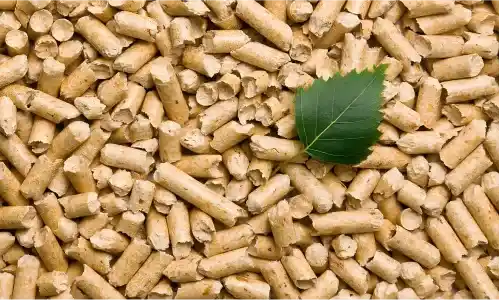
Straw pelletizing is the process of converting agricultural straw into compressed biomass pellets.
The raw material may include:
- Wheat straw
- Rice straw
- Corn stalks
- Barley straw
- Oat straw
- Sorghum stalks
- Rapeseed straw
- Cotton stalks
- Grass and other dry crop residues
Fresh or untreated straw is normally unsuitable for direct pelletizing because it is long, fibrous, lightweight, and difficult to feed consistently. Therefore, the material usually needs to be processed before entering the pellet mill.
During pelletizing, prepared straw particles are fed into a compression chamber. A rotating roller forces the material through holes in a ring die or flat die. Pressure and friction generate heat, while the natural binding properties of lignin and other components help hold the compressed particles together.
The result is a dense pellet with a relatively uniform shape and size.
Depending on the application, straw fuel pellets can commonly be produced in different diameters, such as 6 mm, 8 mm, or 10 mm. The appropriate size depends on the combustion equipment, transportation requirements, and end-user preferences.
Why Turn Agricultural Waste Into Fuel?
Straw has traditionally been considered an agricultural residue rather than a valuable fuel resource. However, it contains combustible organic matter and can be processed into a useful biomass fuel when its properties and quality are properly controlled.
Pelletizing offers several advantages over using loose straw.
Higher Bulk Density
Loose straw occupies a large volume because its fibers contain significant amounts of air. This makes transportation and storage inefficient.
Pelletizing compresses the material into a much denser form. A truck can therefore transport considerably more usable biomass energy in the same volume than it could with loose straw.
Easier Transportation
Straw bales can be large and irregular, while loose straw is difficult to handle mechanically.
Pellets have a standardized size and shape. They can be transported using conveyors, trucks, bulk systems, or bags, depending on the scale of the operation.
More Convenient Storage
Loose agricultural residues require considerable storage space. Pellets can be stacked or stored in silos and warehouses more efficiently.
Properly cooled and dried pellets also have better handling characteristics than freshly compressed material.
More Consistent Fuel
Raw straw varies in moisture, particle size, and composition. Pelletizing creates a more standardized fuel product.
This makes it easier for users to establish feeding and combustion parameters for biomass boilers, furnaces, and heating systems.
Better Agricultural Waste Utilization
Instead of treating straw exclusively as waste, pelletizing creates an opportunity to convert it into a commercial biomass product.
For farms, agricultural cooperatives, biomass fuel producers, and agro-industrial companies, this can create an additional utilization route for crop residues.
How Does Straw Become a Fuel Pellet?
The complete process normally includes several stages:
Straw collection → Cleaning → Bale breaking → Shredding → Drying → Crushing → Pelletizing → Cooling → Screening → Packaging
Not every project requires exactly the same process. The equipment configuration depends on the straw type, initial moisture, contamination level, production capacity, and required pellet quality.
Let’s examine each stage in detail.
1. Straw Collection and Raw Material Preparation
The first stage is collecting agricultural residues from farms or processing facilities.
Straw may arrive in several forms. It can be loose, baled, chopped, or partially processed.
Baled straw is particularly common because baling makes agricultural residues easier to transport from fields to a central processing plant.
However, large bales cannot normally be fed directly into a pellet mill.
A bale breaker or bale opener is therefore often installed at the beginning of the production line.
Its purpose is to separate compressed straw and provide a more continuous material flow to the following equipment.
2. Cleaning the Straw
Agricultural straw can contain unwanted materials such as:
- Soil
- Stones
- Sand
- Metal
- Plastic
- Twine
- Other field debris
These contaminants can damage shredders, hammer mills, conveyors, and pellet mills.
A cleaning system can therefore improve the reliability of the production line.
Magnetic separators are especially useful for removing ferrous metal particles. Screening equipment can also help separate oversized contaminants and unwanted foreign materials.
The cleaner the raw material, the lower the risk of equipment damage and excessive wear.
3. Straw Shredding
Long straw fibers can create serious feeding problems.
If long fibers enter the pellet mill without sufficient size reduction, they can cause bridging, unstable feeding, and uneven compression.
A straw shredder cuts long stalks into shorter pieces.
The objective at this stage is not necessarily to produce very fine powder. Instead, the goal is to reduce fiber length enough for stable downstream processing.
The required particle size depends on the raw material and the design of the pellet mill.
4. Drying Straw
Moisture is one of the most important factors affecting straw pelletizing.
Fresh agricultural residues may contain significantly more moisture than the pelletizing process requires. Excessive moisture can reduce compression efficiency and cause unstable pellet formation.
An industrial rotary dryer machine or other biomass drying system can be used to reduce moisture to an appropriate range.
The exact target depends on the straw species, initial moisture, particle size, environmental conditions, and pellet mill design.
Over-drying should also be avoided. If the material becomes excessively dry, pellet formation may become difficult and dust generation may increase.
Therefore, the drying system should be designed around the actual characteristics of the raw material rather than using one fixed setting for every project.
5. Straw Crushing and Fine Grinding
After drying, the straw may require further size reduction.
A hammer mill or biomass grinder can process shredded straw into a more uniform particle size.
Fine grinding improves material consistency and helps the particles move through the pellet mill more evenly.
However, grinding also consumes electricity. Excessive grinding can increase energy consumption without producing a meaningful improvement in pellet quality.
For this reason, particle size should be matched to the pellet mill, die specification, straw type, and desired pellet diameter.
6. Moisture Adjustment and Material Conditioning
After drying and grinding, the straw should be checked again for moisture.
A stable moisture level is essential for consistent pellet production.
If the material is too dry, it may not bind properly. If it is too wet, the pellet may become soft, sticky, or difficult to cool.
In some production systems, water or steam may be used for conditioning. Conditioning can improve temperature and moisture distribution before compression.
The correct approach depends on the straw composition and the requirements of the pellet mill.
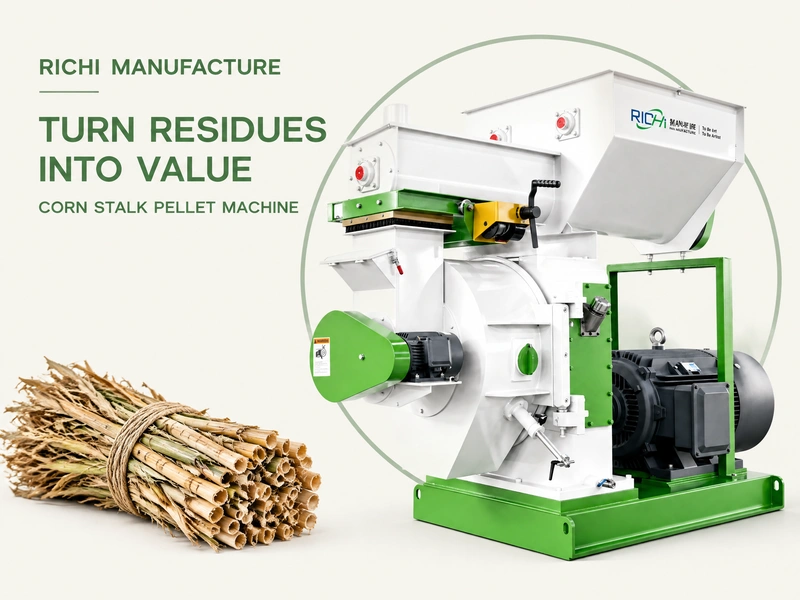
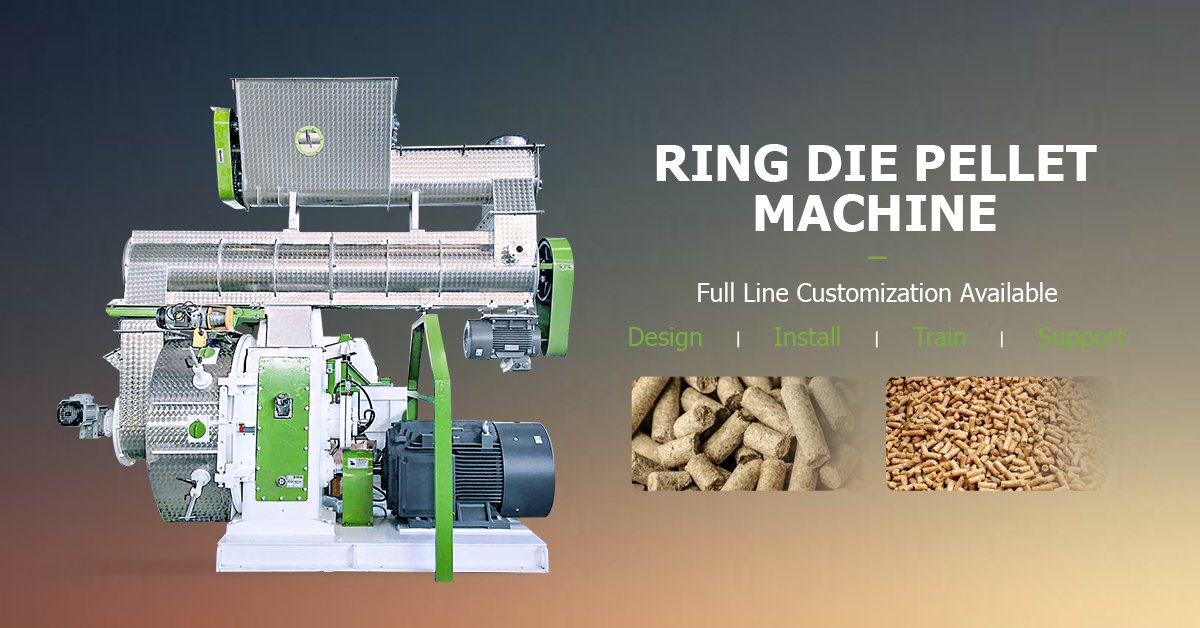
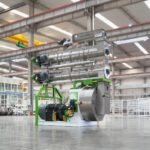
7. Pelletizing With a Straw Pellet Press
The pelletizing stage is the core of the process.
A straw pellet press compresses prepared agricultural residues into dense cylindrical pellets.
In a ring-die pellet mill, material enters the compression chamber and is pressed between rotating rollers and the inner surface of the ring die.
The rollers force the straw through small holes in the die. As the compressed material exits the die, knives cut the continuous material into pellets of the desired length.
(Learn more: https://richipelletizer.com/straw-pellet-machine-for-sale/)
Several physical factors contribute to pellet formation.
Mechanical Pressure
High pressure is required to compress loose straw into a stable pellet.
The required pressure depends on material characteristics, moisture, particle size, die compression ratio, and pellet diameter.
Friction and Heat
Compression generates frictional heat inside the pelletizing chamber.
This heat can soften lignin and help it act as a natural binder.
This is one reason many biomass materials can form pellets without relying on large quantities of synthetic binding agents.
Die Compression Ratio
The die compression ratio is an important parameter when selecting a pellet mill.
Different straw types have different fiber structures and resistance to compression.
A die suitable for one biomass material may not provide the same results with another.
Therefore, die selection should be based on actual raw material tests and production requirements.
Roller and Die Condition
The roller and die are critical wear components.
If the die holes become worn or the roller surface deteriorates, compression efficiency can decline.
This may result in lower production capacity, higher energy consumption, unstable pellet quality, or increased pellet breakage.
Regular inspection and maintenance are therefore essential.
8. Cooling the Fresh Pellets
Freshly produced pellets are hot and may still contain moisture.
They should not normally be packaged immediately after leaving the pellet mill.
A pellet cooler reduces pellet temperature and helps stabilize the product.
Counterflow coolers are commonly used in industrial pellet production because they can provide controlled cooling while removing residual moisture.
Proper cooling also improves pellet hardness and reduces the risk of condensation inside storage bags.
9. Screening the Pellets
After cooling, the pellets can be screened.
Screening separates finished pellets from:
- Fines
- Broken pellets
- Oversized particles
- Unstable material
Fines can often be recycled back into the production process.
This improves product recovery and reduces material waste.
A well-designed screening system is particularly important when pellets are intended for commercial sale because customers generally expect a relatively uniform product with limited fines.
10. Packaging and Storage
The final stage is packaging or bulk storage.
Small producers may use bags, while larger biomass fuel plants may load pellets directly into bulk trucks or storage silos.
Packaging protects pellets from moisture and contamination.
Storage conditions are also important. Biomass pellets should be kept dry and protected from rain, groundwater, and excessive humidity.
Poor storage can cause pellets to absorb moisture, lose strength, generate more fines, and become unsuitable for efficient combustion.
What Makes Straw Suitable for Pellet Fuel?
Straw contains cellulose, hemicellulose, lignin, and other organic components.
These components contain chemical energy that can be released during combustion.
However, straw fuel properties vary significantly according to crop species, growing conditions, soil, harvesting methods, and contamination.
For example, rice straw and wheat straw do not necessarily behave identically during pelletizing or combustion.
This means a commercial pellet plant should not assume that one processing configuration will work equally well for every agricultural residue.
Raw material testing is valuable before finalizing the production line.
Important characteristics include:
- Moisture content
- Ash content
- Particle size
- Fiber length
- Bulk density
- Calorific value
- Chemical composition
- Contamination level
- Pellet durability requirements
How Moisture Affects Straw Pellets
Moisture has a major effect on pellet production.
If straw contains excessive moisture, several problems may occur:
- Poor compression
- Soft pellets
- Increased steam generation
- Higher energy consumption during drying
- Pellet deformation
- Difficult cooling
- Storage problems
If the material is excessively dry, the pellet mill may also struggle to achieve stable pellet formation.
Therefore, moisture management should cover the entire production process rather than only the dryer.
Operators should monitor the material before grinding, before pelletizing, and after cooling.
How Particle Size Affects Pellet Quality
Particle size influences feeding, compression, pellet density, and energy consumption.
Very large particles can make compression difficult.
Extremely fine particles may increase grinding costs and dust generation.
A suitable particle size distribution provides a balance between pellet quality and energy efficiency.
The ideal specification should therefore be determined according to the straw type, pellet diameter, die design, and production capacity.
Why Straw Pellets Are Easier to Handle Than Loose Straw
One of the biggest advantages of pelletizing is improved material handling.
Loose straw is:
- Bulky
- Lightweight
- Irregular
- Difficult to transport efficiently
- Difficult to feed automatically
Pellets are:
- Compact
- Uniform
- Easy to convey
- Easier to weigh
- Easier to package
- Suitable for automated feeding systems
This makes pelletized straw more practical for commercial biomass fuel applications.
Where Can Straw Fuel Pellets Be Used?
Straw pellets can potentially be used in a range of biomass combustion applications, depending on their fuel properties and the requirements of the combustion system.
Potential applications include:
Biomass Boilers
Straw pellets can be used as a solid biomass fuel in appropriately designed boilers.
Industrial Heating
Factories and processing facilities may use biomass pellets for heat generation where compatible combustion equipment is available.
Agricultural Facilities
Farms, greenhouses, grain-processing facilities, and other agricultural operations may use biomass pellets for heating.
Commercial Heating
Some commercial heating systems can use standardized biomass pellets instead of loose agricultural residues.
Combined Biomass Fuel Systems
Some plants may process several agricultural residues into one pellet fuel, provided the raw materials are compatible and the resulting fuel meets the requirements of the combustion system.
What Equipment Is Needed for a Straw Pellet Production Line?
A complete straw pellet production line may include:
- Raw material receiving system
- Bale breaker
- Cleaning equipment
- Straw shredder
- Magnetic separator
- Rotary dryer
- Hammer mill
- Buffer hopper
- Feed conveyor
- Straw pellet press
- Pellet cooler
- Vibrating screen
- Finished-product conveyor
- Packing machine
- Dust collection system
- Electrical control system
The exact equipment configuration should be customized.
For example, a small farm using already-dried chopped straw may require a much simpler system than a commercial plant processing high-moisture baled straw.
How to Choose the Right Straw Pellet Press
Selecting the pellet press is one of the most important decisions when establishing a straw fuel pellet plant.
Several factors should be considered.
1. Raw Material Type
Wheat straw, rice straw, corn stalks, and other residues have different fiber structures.
The machine should be suitable for the actual material being processed.
2. Production Capacity
The required output may range from a small farm-scale system to a large commercial biomass fuel plant.
Capacity should be selected based on raw material availability and expected market demand.
3. Pellet Diameter
The desired pellet diameter affects die design and compression requirements.
Common sizes include 6 mm and 8 mm, but other diameters may be possible depending on the application.
4. Moisture
The pellet mill should be matched with the drying system and expected moisture conditions.
A high-capacity pellet mill cannot compensate for poorly controlled raw material moisture.
5. Die and Roller Design
The die and roller system must withstand continuous compression and abrasive biomass materials.
Wear-resistant components can help maintain stable production over longer operating periods.
6. Automation
Larger plants may benefit from automated feeding, temperature monitoring, lubrication, overload protection, and centralized control.
Automation can reduce manual intervention and improve process consistency.
(visit this site:RICHI Pelletizer)
Common Problems During Straw Pelletizing
Even a well-designed line can experience production problems if operating parameters are not properly controlled.
Pellets Break Easily
Possible causes include unsuitable moisture, insufficient compression, incorrect die specifications, or inadequate cooling.
Low Production Capacity
Possible causes include poor feeding, excessive moisture, unsuitable particle size, die blockage, or insufficient grinding.
High Energy Consumption
High power consumption may result from excessive grinding, inefficient drying, worn components, or unsuitable pelletizing parameters.
Die Blocking
Die blockage can occur when material moisture, particle size, feeding rate, or compression conditions are inappropriate.
Excessive Fines
A high percentage of fines can result from poor pellet formation, insufficient cooling, inadequate screening, excessive handling, or unsuitable raw material conditions.
These problems demonstrate why pellet production should be treated as an integrated process rather than simply a matter of purchasing a pellet machine.
Why a Complete Straw Pellet Line Matters
A pellet press is the core compression machine, but it is only one part of a commercial production system.
A pellet mill cannot solve problems caused by wet straw, oversized fibers, excessive contamination, unstable feeding, or poor cooling.
For example, if the dryer cannot maintain stable moisture, pellet production will also become unstable.
If the hammer mill produces inconsistent particle sizes, the pellet mill may experience uneven feeding.
If the cooler is undersized, freshly produced pellets may enter the packaging system while still too hot.
For this reason, the production line should be designed as a complete system.
A well-balanced line coordinates:
Raw material preparation → Moisture control → Size reduction → Feeding → Compression → Cooling → Screening → Packaging
This approach can improve production stability and make the entire plant easier to operate.
Straw Pelletizing as a Waste-to-Fuel Solution
The main value of straw pelletizing is not simply the production of small cylindrical pellets.
It is the transformation of a difficult-to-handle agricultural residue into a more standardized biomass fuel.
Instead of transporting large volumes of loose straw, producers can densify the material.
Instead of storing irregular agricultural residues, users can handle uniform pellets.
Instead of feeding loose fibers into combustion equipment, users can use a more standardized solid fuel where the combustion system is designed for it.
This makes pelletizing particularly relevant in regions with significant agricultural production and abundant crop residues.
Is Straw Pelletizing Suitable for Every Agricultural Waste?
Not necessarily.
The suitability of a material depends on its physical and chemical properties.
Some residues may have high ash content, high mineral contamination, excessive moisture, or other characteristics that require additional processing or make them less suitable for certain combustion applications.
Therefore, raw material testing should be performed before building a large production plant.
Testing can help determine:
- Required drying capacity
- Appropriate grinding size
- Suitable die compression ratio
- Expected pellet density
- Pellet durability
- Expected production capacity
- Energy consumption
- Fuel properties
This information can then be used to design the equipment configuration.
From Agricultural Residue to Commercial Biomass Fuel
The complete transformation can be summarized in several stages.
Agricultural residue
↓
Collection and transportation
↓
Cleaning and bale breaking
↓
Shredding and size reduction
↓
Drying and moisture adjustment
↓
Fine grinding
↓
Compression in a straw pellet press
↓
Cooling and stabilization
↓
Screening
↓
Packaging or bulk storage
↓
Biomass fuel application
Each stage contributes to the final quality and economics of the product.
The pellet mill creates the compact fuel form, but the upstream and downstream equipment determine whether the pellet mill can operate efficiently and consistently.
Final Considerations Before Building a Straw Pellet Plant
Before investing in a straw pellet production line, several questions should be answered.
First, what type of straw is available?
Second, how much raw material is available throughout the year?
Third, what is the average moisture content?
Fourth, how will the straw be collected and transported?
Fifth, what pellet diameter does the target market require?
Sixth, what production capacity is needed?
Seventh, what type of combustion equipment will consume the pellets?
Eighth, what storage method will be used?
Ninth, what level of automation is appropriate?
Finally, how will equipment maintenance and spare parts be managed?
Answering these questions before equipment selection can prevent many problems during commissioning.
Conclusion
Straw pelletizing provides a practical method for converting agricultural residues into a more compact and manageable biomass fuel. Wheat straw, rice straw, corn stalks, barley straw, and other crop residues can be processed through a sequence of cleaning, shredding, drying, grinding, pelletizing, cooling, screening, and packaging.
At the heart of this process, the straw pellet press compresses prepared biomass into dense pellets by combining mechanical pressure, friction, and the natural binding properties of the material.
However, successful straw pellet production depends on more than the pellet press itself. Moisture control, particle size, raw material preparation, die selection, feeding stability, cooling, screening, and storage all influence the final product.
For farms, agricultural enterprises, biomass fuel manufacturers, and investors located in areas with abundant crop residues, a properly designed straw pellet production line can provide a route for turning underutilized agricultural waste into a standardized biomass fuel.
The most effective approach is to design the complete processing system around the actual raw material, required capacity, pellet specifications, and end-use application. With appropriate equipment selection and process control, agricultural straw can move from being a bulky field residue to becoming a more convenient, transportable, and commercially useful biomass energy resource